Cosmetic Aluminum Alloy Housing
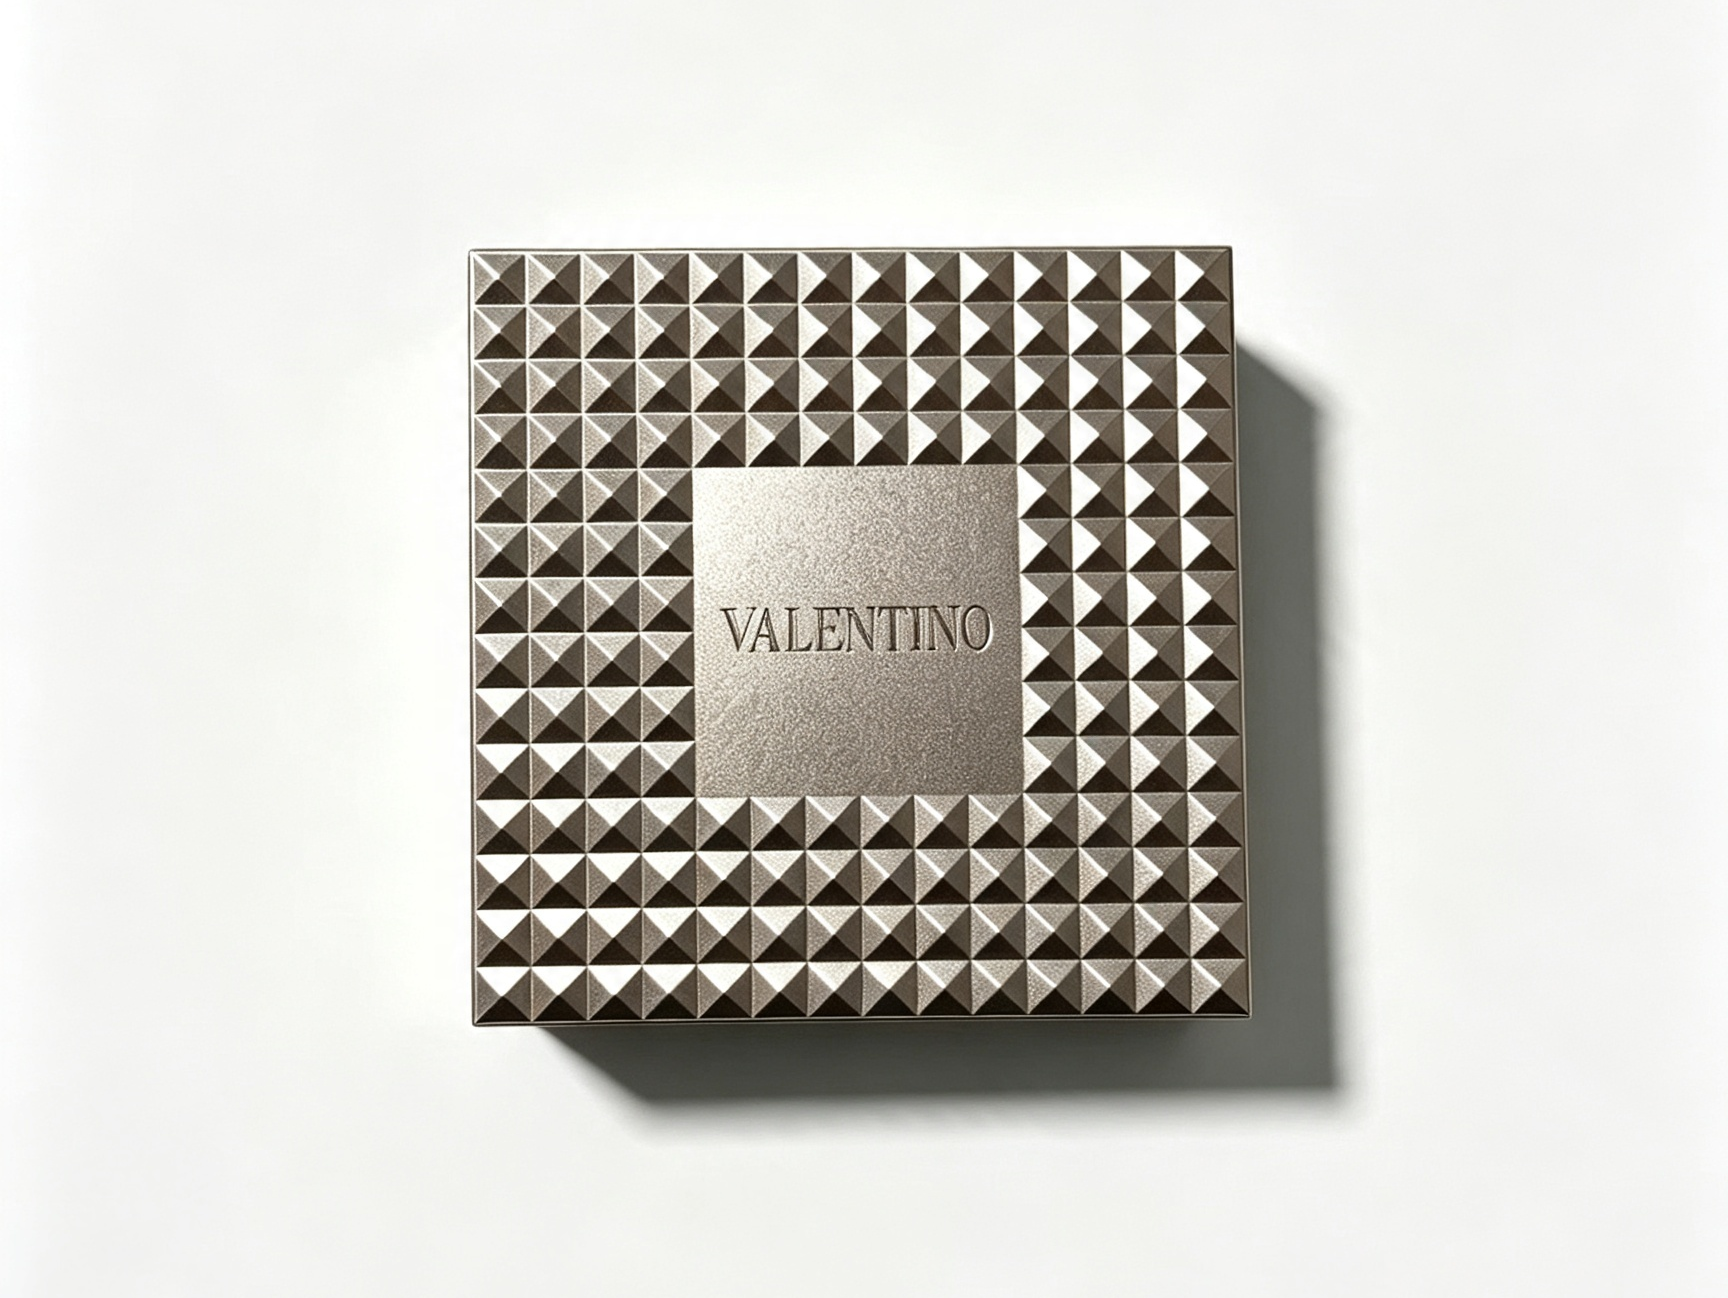
Material: Low-silicon (max 0.5%) Al-Mg custom alloy, anodizable
Surface treatment: Anodizing
Typical customer: premium cosmetics and beauty packaging brands
Anodized die casting only works when the casting is clean enough to skip polishing. This cosmetic housing is cast in a low-silicon Al-Mg alloy, and the finish is agreed with the anodizer before the first production run.
The Challenge
- Dense sharp edges that had to stay crisp. Machining the housing from extrusion held the edges, but the output could not keep up with volume.
- Standard ADC12 / A380 die castings anodize badly, and the finish fell short of what a premium beauty brand will accept.
- A 1.2 mm wall over a large projected area invites cold shuts and entrapped air. Both show up as streaks and mottling after anodizing.
- The edges could not be polished or ground, so the casting itself had to come out clean enough to anodize as cast.
- The anodizing window for die cast aluminum is narrow, and few finishing shops will even quote the work.
Process Approach
- The housing is cast in a custom low-silicon alloy (max 0.5%) rather than ADC12 or A380. Silicon is the element that ruins anodized appearance, so dropping it is what makes a die casting anodizable in the first place.
- Low-silicon alloys flow badly, and the resulting cold shuts and entrapped air show up as streaks after anodizing. Gating and overflow were redesigned, runner cross-sections rebalanced and vacuum die casting added, which lifted casting quality noticeably.
- A silicon-free release agent is used, with spray position and volume controlled and sticking checked on a schedule. That brought the batch reject rate down and stabilised both lead time and first-pass yield.
- Anodizing requirements were agreed with the finishing partner at sampling stage, including cycle time and the handling this alloy needs. Volume production only starts after the first article passes anodizing.
- Re-melt ratio is capped at 30% and the number of re-melt cycles is limited. Overflow and biscuit scrap high in oxide is kept out of the melt, so the alloying elements in this special alloy are not depleted and material performance stays consistent.
About Xiuhui
Dongguan Xiuhui Precision Technology Co., Ltd. is based in Houjie, Dongguan, and specialises in precision structural and cosmetic parts in zinc and aluminum alloys. Thin walls, tight tolerances and plated surfaces are the work we take on, and most of our projects start as a casting problem someone else could not solve. Customer size does not decide whether we engage; the engineering does. Customers and industry peers are both welcome to contact us about zinc and aluminum die casting.
Parts cast and finished on the same lines include the Anodized Aluminum Cosmetic Box and the Anodized Aluminum Electronic Enclosure.