Support Arm
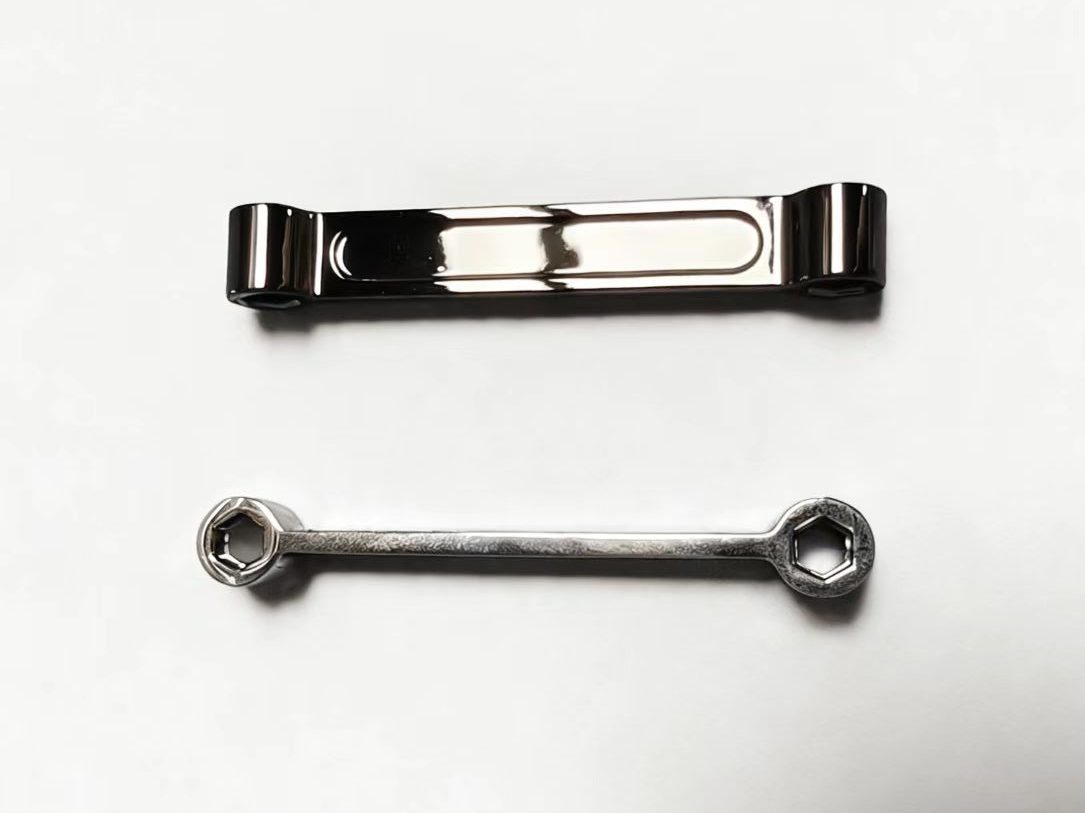
Material: Zinc Alloy Die Casting
Application: Consumer Electronics
Secondary Process: Deburring, Polishing
Surface Treatment: Electroplating
Lead Time: 7-10 days
Product Advantages: 1. Even plating with no strike-through, colour drift or pitting — on a visible part this is the first thing anyone sees, and a pit is also where corrosion starts. Appearance is checked by batch, from raw casting through polishing to plating, not by pulling one or two samples. 2. Bores held to plus or minus 0.03 mm and still correct after plating — plating thickens the wall and closes the hole, so a bore that passes before plating can bind afterwards. We re-measure the bores after plating and ship to that dimension, so the arm goes on without tapping. 3. Cast close to final shape, with only the machining allowance that is actually needed — compared with turning the part from zinc bar stock, cycle time and material loss both drop, and the gap widens with volume. Radii and ribs come out of the die in one piece, avoiding distortion from repeated re-clamping. 4. Polishing and plating under one roof, 7-10 days — no part travelling between suppliers, so a colour or pinhole issue has one owner and rework is fast. Your schedule is not held up by another factory’s queue.
Overview
A support arm looks simple until the joint starts to droop. The bores have to be round and on position, because the clearance between the arm and the pivot decides whether the mounted device stays where it is put. This arm is cast in zinc alloy, polished and electroplated, with the bores held to plus or minus 0.03 mm and the plating kept free of pinholes inside them.
Typical Applications
Display mounts, lighting arms, camera and instrument arms and general equipment mounting hardware. It is finished on the same line as an optical module housing and a luminous data cable housing.
Manufacturing Capability
Arms are cast on zinc machines from 88 to 168 tonnes, then polished and plated. The bore tolerance of plus or minus 0.03 mm is held by controlling the casting and by checking the bore after plating, since a plated layer adds to the wall. Plating coverage inside the bore is inspected for pinholes, because a pore there becomes a corrosion point and a squeak.
Why Work With Xiuhui
Xiuhui has been die casting zinc and aluminum in Dongguan for over 20 years. Mounting hardware fails quietly: nothing breaks, the arm just will not hold its angle. Holding bore size and plating quality together is the whole job, and both are done in house so the two do not get traded off against each other.